OIL & GAS EQUIPMENT | Updated November 2026 | 9 min read
Selecting a vapor recovery unit manufacturer involves more than comparing prices on packaged compressor skids. The right manufacturer must demonstrate verified API Standard 11P compliance, show documented capacity to meet EPA 40 CFR 60 Subpart OOOOb performance requirements, and maintain a direct service network capable of supporting your installation past commissioning. In upstream oil and gas operations, a poorly specified vapor recovery system leaves operators exposed to both regulatory penalty and unplanned downtime, often simultaneously.
Hero Process Solutions, founded in 2011 and headquartered in Kellyville, OK with operations in Midland, TX, designs and manufactures VRUs alongside a full portfolio of combustion and vapor control equipment for the global oil and gas industry. Their field services team provides direct on-site support from initial sizing through commissioning, a critical capability when manufacturers relying on distributor networks cannot mobilize engineers quickly when equipment underperforms.
WHAT YOU’LL LEARN IN THIS GUIDE
- Which API and EPA standards a qualified vapor recovery unit manufacturer must comply with
- How to verify API Standard 11P documentation before finalizing a purchase order
- What EPA 40 CFR 60 Subpart OOOOb requires of operators and their VRU equipment
- Realistic lead times for VRU delivery in today’s market and how to plan around them
- Service capability benchmarks to hold manufacturers to before contract signing
- How VRUs compare to vapor combustors and BTEX condensers for your application
- The right questions to ask any VRU manufacturer during the bidding process
- Common procurement mistakes that create compliance gaps after installation
DIRECT ANSWER: Vapor Recovery Unit Manufacturer
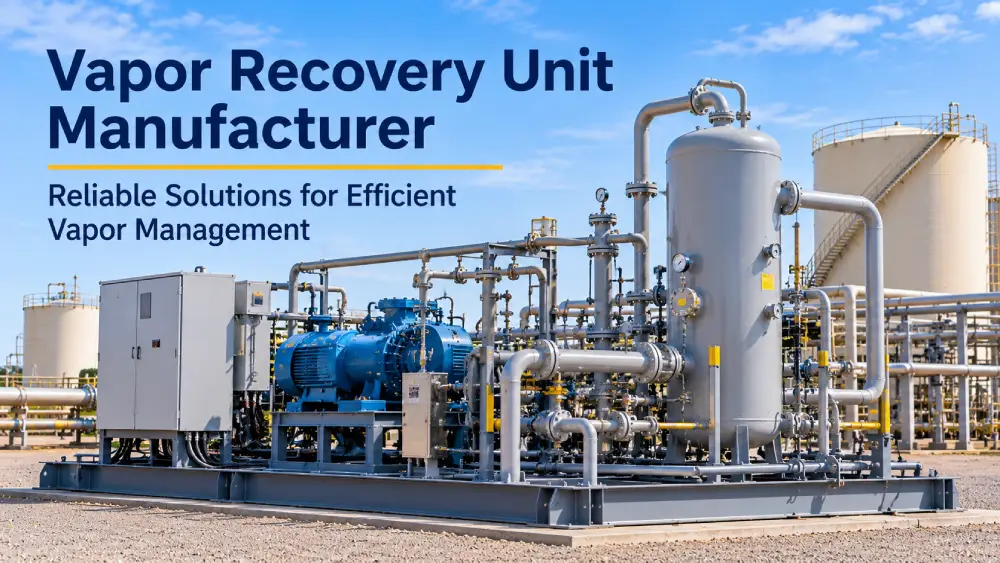
A vapor recovery unit manufacturer designs and builds packaged compressor systems that capture tank battery vapors, compress them, and route them to a sales pipeline or combustion device. Qualified manufacturers build units to API Standard 11P specifications for packaged reciprocating compressors and provide documentation demonstrating compliance with EPA 40 CFR 60 Subpart OOOOb performance thresholds. Operators should verify that the manufacturer holds actual vapor destruction efficiency test data and can provide direct field service support in their operating region before finalizing any equipment purchase.
1. What a Qualified Vapor Recovery Unit Manufacturer Must Demonstrate
Not all VRU manufacturers operate at the same technical level. The oil and gas industry has seen a significant growth of packaged compressor assemblers who source components from multiple vendors and offer minimal engineering support after the sale. Before entering a procurement process, operators should require documented evidence across four areas:
- API 11P Certification: The manufacturer must build to API Standard 11P for packaged reciprocating compressors. This standard covers design, materials, fabrication, inspection, and testing requirements for compressor packages used in oil and gas service. Ask for the certification documentation at bid stage, not after award.
- Vapor Destruction Efficiency Documentation: Under EPA OOOOb, operators must use emissions control devices that meet specific destruction efficiency thresholds. A manufacturer should provide actual test data, not just design estimates from simulation software.
- Application-Specific Sizing: VRUs are sized to specific gas flow rates, composition, inlet pressure, and temperature conditions. A qualified manufacturer uses process simulation to verify sizing before fabrication, not rule-of-thumb estimates based on generic tank categories.
- Manufacturing Traceability: A full bill of materials, material test reports, and inspection records should be available at equipment delivery. This documentation is necessary for regulatory compliance files and for any future warranty claims.
KEY INSIGHT
API Standard 11P covers packaged reciprocating compressors specifically used in gas compression service in the oil and gas industry. Operators who do not require API 11P compliance during procurement often discover that components sourced from non-certified suppliers fail under cyclic loading conditions typical of tank battery vapor streams, which vary significantly in flow rate and composition throughout the production day. Retrofitting non-compliant components after delivery typically costs more than specifying correctly at bid stage.
2. API Standard 11P: What It Covers and Why Vapor Recovery Unit Manufacturers Must Follow It
API Standard 11P establishes minimum design and performance requirements for packaged reciprocating compressors. For vapor recovery unit manufacturers, this standard governs critical components including the compressor frame, cylinder design, pulsation control systems, driver selection, and control panel specifications. Manufacturers who build outside API 11P often use undersized components or omit pulsation analysis, which leads to premature valve failure and vibration fatigue on piping connections in tank battery service.
Several specific API 11P requirements affect VRU performance in storage tank vapor recovery service:
- Pulsation Analysis: API 11P requires a pulsation analysis for packaged compressors operating above certain horsepower thresholds. Tank battery vapor streams typically exhibit irregular flow patterns throughout the production day. Without proper pulsation control, cylinder unloaders and valves experience accelerated wear that shortens service intervals significantly.
- Driver-Compressor Compatibility: The standard specifies requirements for coupling and power transmission components. Mismatched driver-compressor selections are a common failure mode in non-certified packages and a frequent root cause of premature overhaul requirements.
- Pressure Vessel Code Compliance: Heat exchangers, intercoolers, and suction scrubbers within the VRU package must meet applicable pressure vessel codes per API 11P requirements. Verify that the manufacturer provides ASME stamp documentation for all pressure-containing components at delivery.
For operators managing BTEX-containing vapor streams, API 11P compliance is particularly important because benzene, toluene, ethylbenzene, and xylene compounds degrade standard seal materials and require specific metallurgical selections. Hero Process Solutions’ BTEX condenser systems are engineered in coordination with VRU sizing to handle compound streams that contain elevated aromatic hydrocarbon content without accelerated component degradation.
3. EPA 40 CFR 60 Subpart OOOOb: What Operators Must Verify Before Purchase
EPA 40 CFR 60 Subpart OOOOb, the Standards of Performance for New, Reconstructed, and Modified Sources in the Oil and Natural Gas Sector, establishes specific emissions control requirements for storage vessels at oil and natural gas production operations. Under these rules, operators of affected storage tanks must route vapor streams to a qualifying control device, which can include a VRU connected to a sales pipeline, a vapor combustor, or a flare system meeting the rule’s performance thresholds.
A qualified vapor recovery unit manufacturer should be able to provide documentation demonstrating that their equipment configuration can meet Subpart OOOOb requirements for your specific tank battery. This includes three key documentation requirements:
- Control Device Efficiency Documentation: Subpart OOOOb specifies minimum destruction efficiency requirements for vapor control devices. Operators must verify that the VRU, when connected to a combustion device for backup, meets or exceeds the required threshold for the regulated pollutants at your facility.
- Monitoring and Recordkeeping Compliance: The rule requires specific monitoring of control device performance. Manufacturers should supply VRUs equipped with appropriate monitoring points that satisfy Subpart OOOOb recordkeeping requirements, including flow metering and operational status indicators.
- Alternative Compliance Path Verification: For operators who route captured vapor to a sales line, the VRU itself may satisfy compliance without a separate combustion device, provided the system operates continuously and all captured gas is delivered to the pipeline at compliant pressures. The manufacturer must confirm their system design supports this compliance path for your specific installation.
When a VRU cannot fully recover all vapor volume during periods of peak production, operators need a documented backup combustion device. Hero Process Solutions’ vapor combustors are engineered to operate as backup devices when VRU capacity is exceeded or during scheduled maintenance downtime, maintaining continuous regulatory compliance. For comprehensive EPA OOOOb compliance documentation, the interaction between the VRU and any backup combustion device must be clearly defined in the facility’s compliance records and Notification of Compliance Status submissions.
CRITICAL RULE
Under EPA 40 CFR 60 Subpart OOOOb, operators of affected storage vessels must have their control device operating at all times vapors are being routed to it. A VRU that routinely exceeds its design inlet flow capacity and allows vapor bypass to atmosphere places the operator in direct violation of this continuous operation requirement. Size your VRU to peak vapor generation rates observed during initial production, not average flow conditions measured after the well has begun declining.
4. Lead Time Realities: Why VRU Delivery Takes Longer Than Expected
VRU lead times in the current market range from 12 to 24 weeks for standard packaged units, with custom configurations requiring additional fabrication time beyond that range. Several factors drive these timelines that procurement teams consistently underestimate during initial project planning:
- Compressor Component Availability: Reciprocating compressor frames, cylinders, and valve sets from established manufacturers carry their own production lead times that the VRU packager cannot compress. Extended lead times on major compressor OEM components cascade through the entire build schedule without warning.
- Control Panel Fabrication: Instrumentation, control panels, and SCADA integration components often have separate lead times from electrical component suppliers. Custom panel configurations for remote telemetry or specific operator SCADA platforms add additional shop time beyond the panel manufacturer’s standard backlog.
- Engineering Review Cycles: Subpart OOOOb compliance documentation, HAZOP reviews, and third-party inspection requirements for jurisdictions like the Texas Railroad Commission add time to the pre-fabrication phase that many operators do not account for in their schedule.
- Shop Capacity Constraints: Manufacturers running at high shop utilization during active drilling seasons may have limited availability for new orders even after all components are on hand. Capacity constraints are rarely disclosed proactively at bid stage.
Operators who contact a vapor recovery unit manufacturer only after receiving an EPA notice of violation or approaching a permit compliance deadline typically find that standard lead times make compliance within 60 days impossible. Planning VRU procurement 6 months ahead of facility startup or permit modification is the appropriate minimum planning horizon for standard configurations.
5. Service Capabilities to Demand Before You Commit to a Vapor Recovery Unit Manufacturer
The VRU purchase decision should weight post-sale service capabilities as heavily as initial equipment specifications. A manufacturer’s service capability directly affects equipment uptime and your facility’s compliance continuity. Specifically, operators should verify the following before signing a purchase order:
- Regional Field Service Coverage: Confirm the manufacturer has direct field service technicians in your operating region, not just authorized dealers who resell service contracts. For Permian Basin and Mid-Continent operators, service response within 24 to 48 hours of an emergency call is a realistic benchmark to hold manufacturers accountable to in contract terms.
- Spare Parts Availability: Valve sets, packing, piston rings, and suction-discharge valves are high-wear items on reciprocating VRU compressors. Verify that the manufacturer stocks these parts at a regional location, not only at a central warehouse with 3 to 5 day shipping lead times that leave your facility out of compliance while waiting for parts.
- Commissioning Support: Initial VRU startup requires careful adjustment of unloaders, pressure controls, and compressor speed to match actual vapor generation rates. Manufacturers who ship equipment without direct commissioning support leave operators guessing on initial settings, which frequently results in valve damage and early failures within the first 500 operating hours.
- Operational Training and Safety Certification: Operators and maintenance staff should receive documented training on routine service intervals, valve inspection procedures, and early fault indicators. Field technicians working on pressurized equipment must comply with applicable OSHA oil and gas safety standards; confirm your manufacturer’s service team holds current certifications relevant to your operating jurisdiction.
Hero Process Solutions provides integrated field services directly from their technical team, not through a subcontracted dealer network. Their field services operations cover commissioning, scheduled maintenance, and emergency response for VRU and combustion equipment installations across their customer base throughout the Mid-Continent and Permian Basin regions.
6. VRU vs. Vapor Combustor vs. BTEX Condenser: Selecting the Right Emissions Control Technology
The choice between a VRU, a vapor combustor, and a BTEX condenser system depends on gas composition, sales pipeline proximity, vapor volume, and the economics of product recovery versus combustion. The table below compares the three primary technology options for storage tank vapor control:
| Technology | Best Application | Regulatory Compliance Path | Key Limitation |
|---|---|---|---|
| Vapor Recovery Unit (VRU) | High-volume storage tanks with recoverable product value in the vapor stream; facilities with sales pipeline access | EPA OOOOb: captured vapor routed to sales line satisfies continuous operation requirement directly | Requires sales pipeline connection within economical compression range; unsuitable for isolated locations without gathering line access |
| Vapor Combustor Unit (VCU) | Low-to-moderate vapor flow where product recovery economics do not justify VRU capital cost | EPA OOOOb: meets destruction efficiency requirements when operating above 98% DRE; requires reliable pilot ignition | Destroys product value; adequate BTU content in the vapor stream required for stable flame; pilot reliability is the primary operational concern |
| BTEX Condenser System | Vapor streams with high benzene, toluene, ethylbenzene, or xylene content requiring liquid recovery before combustion | Reduces mass emissions load; typically deployed upstream of a VCU or flare as a pre-treatment stage | Adds capital and operating cost; requires liquid handling and disposal plan for recovered condensate |
Hero Process Solutions manufactures all three technology types and can run the process analysis needed to determine which configuration meets your regulatory requirements at the lowest total cost of ownership. Their engineering team at Kellyville, OK evaluates inlet vapor composition, flow rate variability, and pipeline access to specify the correct equipment combination. Learn more about their full product line and engineering approach on the Hero Process Solutions about page.
7. Questions to Ask a Vapor Recovery Unit Manufacturer Before Signing
Procurement managers should use these six questions to evaluate manufacturer qualifications during the bidding process. Require written answers, not verbal commitments during sales calls:
- Can you provide API Standard 11P documentation for the compressor package configuration you are quoting, including pulsation analysis if applicable?
- What is your current shop lead time for this configuration, and which components are on the critical path for delivery?
- Do you have direct field service technicians permanently stationed in our operating region, or do you use a dealer or distributor network for service?
- What is your documented vapor destruction efficiency for the combustion device we will use as backup, and how does it satisfy Subpart OOOOb performance requirements?
- Can you supply process simulation documentation confirming this VRU is sized for our peak vapor generation rates, not average flow conditions?
- What spare parts do you recommend we stock on-site, and what are your current supply lead times for high-wear components like valve sets and packing?
A qualified manufacturer should be able to answer each of these questions directly and in writing before you sign a purchase order. Vague or deferred answers on API compliance, field service availability, or lead times indicate a manufacturer operating as an assembler rather than a design-and-build engineering firm. For operators who need combustion solutions alongside vapor recovery, Hero Process Solutions’ flare systems catalog and VRU line share the same engineering team, ensuring full compatibility between both equipment sets from a single source.
Common Vapor Recovery Unit Manufacturer Selection Mistakes
| Mistake | Why It Hurts Operations and Compliance | Fix |
|---|---|---|
| Sizing VRU to average flow rather than peak vapor generation | Causes vapor bypass during peak production periods, creating Subpart OOOOb continuous operation violations and potential NOV exposure | Require process simulation documentation at peak load conditions; size for maximum expected vapor rate at the highest producing tank in the battery |
| Selecting a manufacturer without regional field service presence | Emergency response delays of 3 to 5 days create extended compliance gaps and production losses that accumulate quickly during extended downtime | Require written confirmation of field technician location and a maximum emergency response time commitment as a contract term |
| Not requiring API 11P compliance documentation at bid stage | Non-certified compressor components fail under cyclic loads typical of tank battery vapor streams, creating premature overhaul requirements and warranty disputes | Make API 11P documentation a bid submittal requirement, not a post-award deliverable; reject bids that cannot provide it upfront |
| Accepting delivery timelines without critical path documentation | Long-lead compressor components cause schedule slippage that operators only discover 6 to 8 weeks into a build when it is too late to source alternatives | Request a build schedule identifying all long-lead items and their current availability at bid acceptance, with a written commitment to notify you within 5 days of any schedule change |
| Ignoring BTEX content in the inlet vapor stream specification | BTEX compounds degrade standard packing and seal materials, causing early failures that void manufacturer warranties and create unplanned downtime during periods of high production | Provide a full vapor composition analysis including BTEX content and concentration at bid stage; require the manufacturer to confirm material selections are compatible with your specific stream |
Internal Linking Plan
| # | Anchor Text | Target URL | Placement Section |
|---|---|---|---|
| 1 | vapor recovery system | https://heroprocesssolutions.com/vapor-recovery-systems/ | Opening paragraph |
| 2 | field services | https://heroprocesssolutions.com/field-services/ | Second paragraph (HPS intro) |
| 3 | BTEX condenser systems | https://heroprocesssolutions.com/btex-condenser-systems/ | Section 2 (API 11P) |
| 4 | vapor combustors | https://heroprocesssolutions.com/combustors/ | Section 3 (EPA OOOOb) |
| 5 | EPA OOOOb compliance | https://heroprocesssolutions.com/oooob-c/ | Section 3 (EPA OOOOb) |
| 6 | about page | https://heroprocesssolutions.com/about/ | Section 6 (technology comparison) |
| 7 | flare systems | https://heroprocesssolutions.com/flares/ | Section 7 (questions to ask) |
External Linking Plan
| # | Anchor Text | Target URL | Placement Section |
|---|---|---|---|
| 1 | API Standard 11P | https://www.api.org/products-and-services/standards | Direct Answer Block |
| 2 | EPA 40 CFR 60 Subpart OOOOb | https://www.ecfr.gov/current/title-40/chapter-I/subchapter-C/part-60/subpart-OOOOb | Direct Answer Block |
| 3 | OSHA oil and gas safety | https://www.osha.gov/oil-gas | Section 5 (service capabilities) |
Article Summary: Key Takeaways on Vapor Recovery Unit Manufacturers
- A qualified vapor recovery unit manufacturer must provide API Standard 11P compliance documentation for all packaged compressor components before purchase order placement.
- EPA 40 CFR 60 Subpart OOOOb requires continuous control device operation; VRU sizing must be based on peak vapor generation rates, not average flow conditions.
- VRU lead times in the current market range from 12 to 24 weeks for standard configurations, making early procurement planning essential for permit compliance deadlines.
- Regional field service presence, not just a national dealer network, is a critical post-sale requirement that should be confirmed in writing before signing any contract.
- BTEX content in the inlet vapor stream requires specific metallurgical selections in compressor seals and packing; operators must provide full composition analysis at bid stage.
- The choice between VRU, vapor combustor, and BTEX condenser system depends on gas composition, sales pipeline access, vapor volume, and the economics of product recovery vs. combustion.
- Pulsation analysis per API 11P is required for compressor packages above specific horsepower thresholds; manufacturers who skip this step create valve and piping failures under field conditions.
- Operators should require process simulation documentation confirming VRU sizing before fabrication begins, not just a generic capacity rating from the manufacturer’s standard product catalog.
- Hero Process Solutions manufactures VRUs, vapor combustors, BTEX condensers, and flare systems from a single engineering source, enabling compatible equipment specification across the full vapor control system.
- Ask every VRU manufacturer six specific questions in writing before bidding closes: API 11P documentation, lead time critical path, regional service technician location, combustion device DRE, peak-load sizing simulation, and spare parts lead times.
Frequently Asked Questions
What is API Standard 11P and why does it matter for vapor recovery units?
API Standard 11P is the American Petroleum Institute’s standard for packaged reciprocating compressors used in oil and gas service. It establishes minimum design, materials, fabrication, inspection, and testing requirements for the complete compressor package, including the compressor frame, cylinders, pulsation control systems, drivers, and auxiliary components. For vapor recovery unit manufacturers, this standard matters because tank battery vapor streams impose cyclic loading conditions that non-certified compressor components routinely fail under, resulting in early valve failures, seal degradation, and vibration-induced piping fatigue that require costly unplanned overhauls.
How long does it take to get a vapor recovery unit delivered?
Standard VRU packages from established manufacturers currently require 12 to 24 weeks from purchase order placement to delivery. This timeline includes compressor OEM component procurement, VRU package fabrication, control panel assembly, testing, and shipping logistics. Custom configurations with non-standard instrumentation, SCADA integrations, or specialized compression ratios for high-pressure sales lines add additional time beyond the standard range. Operators facing EPA compliance deadlines should plan VRU procurement a minimum of 6 months before the required in-service date to avoid schedule risk from component availability delays.
Does an EPA OOOOb-affected storage tank require a vapor recovery unit specifically?
No. EPA 40 CFR 60 Subpart OOOOb requires that vapors from affected storage vessels be controlled by a qualifying device, but it does not mandate a vapor recovery unit specifically. Operators can meet the rule’s requirements using a VRU connected to a sales pipeline, a vapor combustor meeting the required destruction efficiency threshold, or a flare system that satisfies OOOOb’s combustion efficiency requirements. The optimal compliance path depends on the facility’s access to a sales pipeline, the economic value of the recovered vapor, and the BTU content of the vapor stream, which affects the feasibility of combustion-based control.
What is the difference between a vapor recovery unit and a vapor combustor?
A vapor recovery unit compresses captured tank battery vapors and routes them to a sales pipeline, recovering the product value of the gas. A vapor combustor unit thermally destroys those same vapors using a controlled combustion process, meeting EPA OOOOb destruction efficiency requirements but consuming the gas rather than selling it. VRUs are economical when vapor volume is sufficient to generate meaningful revenue and a sales pipeline is accessible. Vapor combustors are typically more cost-effective for low-to-moderate vapor volumes, remote locations without pipeline access, or facilities where the vapor composition makes compression uneconomical due to high water or CO2 content.
How is a vapor recovery unit sized for a tank battery?
VRU sizing begins with a vapor generation analysis that accounts for tank throughput, crude API gravity, operating temperature, tank pressure set points, and flash gas volumes at each stage of separation. The compressor package must be sized to handle peak vapor generation rates, which occur during high-production periods and warm ambient temperature conditions when vapor pressure increases. Qualified vapor recovery unit manufacturers use process simulation software to model the inlet conditions across the expected range of operating scenarios, then select compression ratios, horsepower, and stage configurations to maintain adequate suction pressure control without exceeding design flow limits during peak vapor events.
What field service intervals should I expect for a reciprocating VRU compressor?
Standard service intervals for reciprocating VRU compressors in tank battery service typically include valve inspections at 1,500 to 2,000 operating hours, packing replacement at 2,000 to 4,000 hours depending on gas composition and suction pressure variability, and oil analysis and change intervals specified by the compressor OEM, typically every 1,000 to 2,000 hours. BTEX-containing streams shorten packing life and require more frequent inspection. Operators should establish a preventive maintenance schedule with the manufacturer at commissioning and confirm that the manufacturer’s regional service team can perform these intervals within the response times specified in the service agreement.